How to Arrange Batch Delivery and Safety Stock for CNC Parts
The core of arranging batch delivery and safety stock is to split a single large order into multiple smaller shipments and maintain buffer inventory on either the buyer's or supplier's side to address common issues in CNC machining such as material arrival delays, tool life fluctuations, and quality re-inspection needs. For overseas buyers, this mechanism prevents a single defective batch from halting the entire production line and reduces the financial pressure of warehousing. The arrangement should be determined based on part type, final assembly takt time, and shipping conditions; there is no one-size-fits-all answer.
Key Takeaways
Split deliveries reduce quality risk
Splitting a single large order into multiple smaller shipments avoids halting the entire production line if one batch has quality issues, and allows process drift to be detected early.
Safety stock is calculated based on data
Safety stock levels need to account for average daily demand, lead time, and a risk factor for stockouts. The formula is average daily demand multiplied by (maximum lead time minus average lead time) multiplied by the risk factor.
Supplier and buyer inventory differ
Supplier-side inventory consists of prepared materials and semi-finished goods to shorten lead times, while buyer-side inventory consists of finished goods to absorb lead time fluctuations. This can be coordinated through VMI or consignment models.
Contracts should specify split deliveries and inspection
Contracts should cover delivery dates, quantities, payment terms, and delay penalties for each batch, and stipulate that subsequent batches are only initiated after the first batch passes verification. Sampling rates should be dynamically adjusted based on criticality.
Why Do CNC Parts Need Batch Delivery Instead of One-Time Full Shipment?
Batch delivery for CNC precision parts is adopted to reduce the overall impact of a single batch's quality anomaly on the buyer's production line. A one-time full shipment may seem to simplify logistics, but if that batch has issues such as out-of-tolerance dimensions, surface roughness not meeting Ra 0.3 µm, or material cracks, the buyer faces the risk of returning or scrapping the entire batch. Batch delivery allows the buyer to release subsequent orders only after the initial batches pass incoming inspection and process validation. For the machining side, batching also means that process drift such as tool wear and thermal deformation can be detected early rather than accumulating until the final batch. In practice, the buyer can agree with the supplier on the shipment ratio per batch based on the quantity per batch, unit value, and final assembly cycle, for example, 30% for the first batch, 40% for the middle, and 30% for the final batch, with time reserved for inspection and feedback between batches.
What Parameters Should Be Used to Calculate Safety Stock Levels?
To calculate safety stock levels, the buyer needs to grasp three key parameters: average daily demand, supplier lead time, and an acceptable stockout risk factor. For CNC parts, lead time typically includes material procurement, rough machining, finishing, inspection, and sea or air freight, which can total several weeks, so safety stock often needs to cover one to two full lead time cycles. A simplified formula the buyer can use is: Safety Stock = Average Daily Demand × (Maximum Lead Time − Average Lead Time) × Risk Factor. The risk factor is adjusted based on the criticality of the part; for example, brake system parts supplied by Tier-1 suppliers or critical medical device components should have a higher factor than general decorative parts. Material characteristics also affect stock levels; softer materials like copper and aluminum have higher machining stability and can be slightly lower, while FRP and special alloys are recommended to have higher buffers due to more machining variables.

What Is the Difference Between Supplier-Side and Buyer-Side Safety Stock?
Supplier-side safety stock refers to the buffer of materials, semi-finished goods, or work-in-progress that the machining factory prepares in advance after confirming an order, with the aim of shortening the lead time after formal production begins. Buyer-side safety stock is the finished goods stored in the buyer's own warehouse or a third-party warehouse after receipt, serving to absorb supplier lead time fluctuations and shipping delays. The cost bearers are different, but both are part of overall supply chain resilience. For the buyer, if the supplier is willing to maintain a certain level of inventory in their factory, the buyer's stock level can be correspondingly reduced; conversely, if the supplier only procures materials after receiving an order, the buyer must increase their own buffer. In practice, both parties can agree in the contract on a VMI (Vendor Managed Inventory) or consignment model, where the supplier replenishes based on the buyer's consumption pace, but it must first be confirmed that the supplier has the corresponding warehousing space and shipping scheduling capability.
How are delivery frequency and batch size determined?
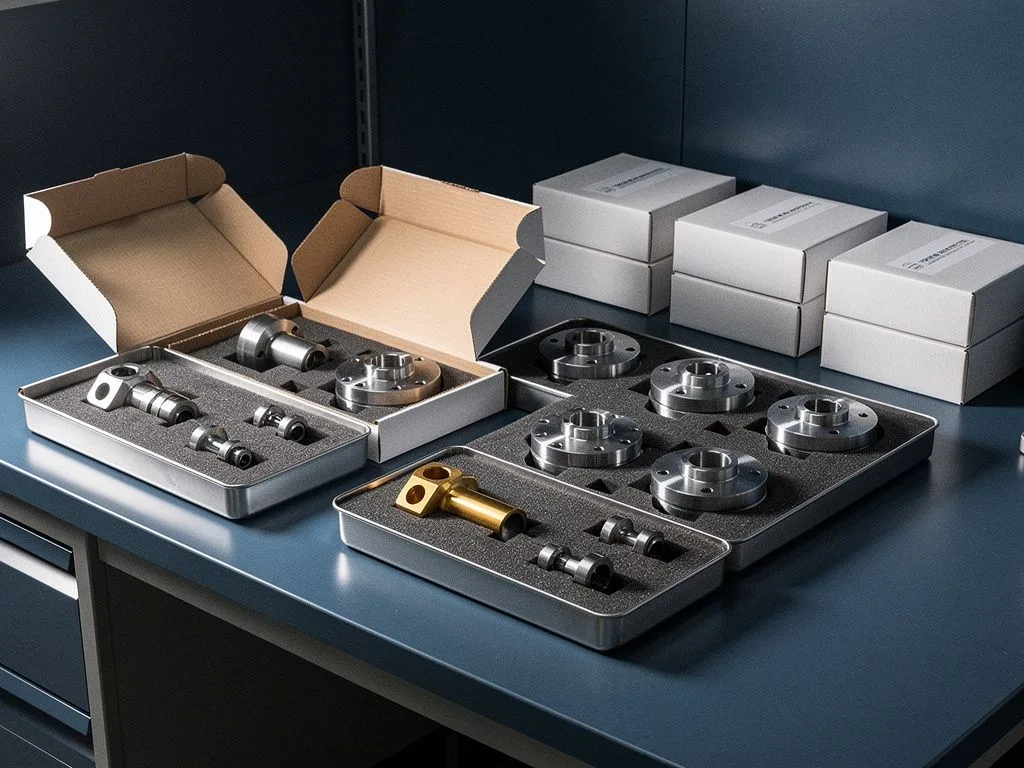
The frequency of partial shipments and the batch size should be determined by balancing the consumption rate of the end assembly line against the cost per shipment. For example, if a buyer needs 5,000 units per month, a common arrangement is five batches of 1,000 units each. If the batch size is too small, the unit cost of transportation and customs clearance rises; if it is too large, the risk-spreading benefit of splitting deliveries is lost. For CNC machining, batch size also affects tool path planning and changeover frequency. For instance, when machining small-diameter parts on a Swiss-type lathe, a batch of 500 to 2,000 units can usually be completed without a changeover, helping to maintain tolerance consistency. Buyers should provide estimated annual usage, batch ratios, and first-delivery requirements during the quotation stage so suppliers can assess production scheduling feasibility.

What batch and inventory terms should be specified in the contract?
Contract terms for partial shipments and safety stock should cover at least four items: delivery date for each batch, quantity per batch, payment terms after inspection approval, and penalties or flexibility clauses for late delivery. Each batch's delivery date should be specified to the week or day, avoiding vague terms like 'ship in batches' without a schedule. The quantity per batch should allow a ±10% flexibility to account for machining yield and material utilization. Each batch should be accompanied by an inspection report before shipment, including at least key dimension measurements, surface roughness records, and material certificates. For buyers, the most critical clause is the right to withhold subsequent batches until the first batch passes verification, which can prevent quality issues at the source. If safety stock is managed under a VMI model, additional terms are needed for inventory ownership transfer timing, stocktaking frequency, and obsolete material return procedures to avoid disputes.
How should the sampling inspection rate be set for partial shipments?
The sampling inspection rate for partial shipments should be adjusted dynamically based on part criticality and first-batch verification results, rather than using the same rate for every batch. For the first batch, full inspection or a high sampling rate is recommended, such as AQL 0.65 or a stricter sampling plan, to establish a process capability baseline. If the first batch meets yield and CPK targets, subsequent batches can gradually reduce the sampling rate to AQL 1.0 or 1.5, but critical dimensions should still be measured 100%. For CNC precision parts, critical dimensions typically include hole diameter, threads, mating surfaces, and Ra surface roughness; these should not be subject to reduced inspection intensity due to batching. Buyers may also require suppliers to provide SPC control charts and MSA/GR&R records before each shipment to confirm measurement system stability before adjusting inspection tightness.
Six items buyers should prepare when arranging partial shipments and safety stock
Estimated annual usage and batch ratios
Provide the estimated annual quantity, first-batch and subsequent-batch ratios, allowing suppliers to assess production scheduling and material procurement feasibility.
End assembly rate and delivery milestones
Specify monthly or weekly assembly demand and the latest arrival date, serving as the basis for calculating partial delivery schedules.
List of critical dimensions and inspection items
List dimensions that require 100% measurement and sampling items, distinguishing between full inspection and sampling scope and AQL levels.
Material specifications and special processing requirements
Indicate material grade, heat treatment, and surface treatment requirements to prevent suppliers from changing material sources between batches.
Shipping method and customs documentation requirements
Specify sea or air freight, any special packaging needs, and the format of inspection reports or certificates of origin to accompany each batch.
Flexibility clauses and abnormal handling procedures
Define contact points, response times, and return/exchange procedures for delivery delays, quantity shortages, or quality issues.
What are the common misconceptions about split deliveries and safety stock?
Buyers often make three common mistakes when arranging split deliveries and safety stock. First, they treat split deliveries as a purely logistical exercise, ignoring the need for process consistency between batches, which can result in noticeable differences between the initial batch and subsequent ones. Second, safety stock levels are set based on intuition rather than data, leading to shortages during peak seasons and excess inventory during slow periods. Third, contracts often fail to specify the right to withhold subsequent batches until the first batch has passed inspection, making it difficult to trace quality issues when they arise. Another frequent issue is placing the entire safety stock burden on the buyer without negotiating VMI or consignment arrangements with the supplier, which concentrates financial pressure and drives up warehousing costs. To avoid these pitfalls, the split ratio, inventory allocation, and inspection procedures should be clearly discussed during the RFQ stage and formalized in the contract, rather than relying on verbal agreements.
FAQ
Why should CNC parts be delivered in batches instead of all at once?
Batch delivery is meant to reduce the overall impact of a quality issue in a single batch on the buyer's production line. If all parts are shipped at once and problems such as out-of-tolerance or material cracks occur, the buyer faces the risk of returning the entire shipment. Batch delivery allows the buyer to release subsequent orders only after the initial batches pass inspection, and the machining side can also detect process drift such as tool wear early.
How should safety stock levels be calculated?
Safety stock = average daily demand × (maximum lead time − average lead time) × risk factor. Lead time includes material procurement, machining, inspection, and transportation, and can be several weeks, so inventory should cover one to two full lead time cycles. The risk factor is adjusted based on part criticality; Tier-1 brake systems or critical medical parts should have a higher factor.
What is the difference between supplier-side and buyer-side safety stock?
Supplier-side inventory is materials, semi-finished goods, or work-in-progress that the machining facility prepares in advance to shorten lead times after formal production begins. Buyer-side inventory is finished goods stored at the buyer's own or a third-party warehouse after receipt, used to absorb lead time fluctuations and transportation delays. If the supplier is willing to maintain inventory, the buyer-side inventory can be reduced; otherwise, the buyer needs to increase its own buffer.
How are the frequency and quantity per batch for split deliveries determined?
This should balance the consumption rate of the final assembly line against the cost per shipment. If monthly demand is 5,000 units, a common configuration is five batches of 1,000 units each. Too few units per batch increases per-unit transportation and customs costs, while too many defeats the purpose of risk diversification. When requesting a quote, provide annual usage, batch split ratio, and initial delivery date requirements.
What batch and inventory clauses should be specified in the contract?
The contract should cover delivery dates, quantities per batch, payment terms after inspection, and delay penalties. Each batch's delivery date should be specified to the week or day, with a ±10% flexibility in quantity. Each shipment should include an inspection report, and the right to initiate subsequent batches only after the first batch passes verification should be agreed. For VMI models, ownership transfer timing and obsolete stock return mechanisms need to be separately defined.
Need an evaluation of split delivery and inventory allocation for your parts?
Please send your annual usage, split ratio, and key dimension requirements to [email protected], or call +886-4-2534-5219. The Yuan Shun Li CNC machining team will provide split scheduling recommendations based on your part type and material.