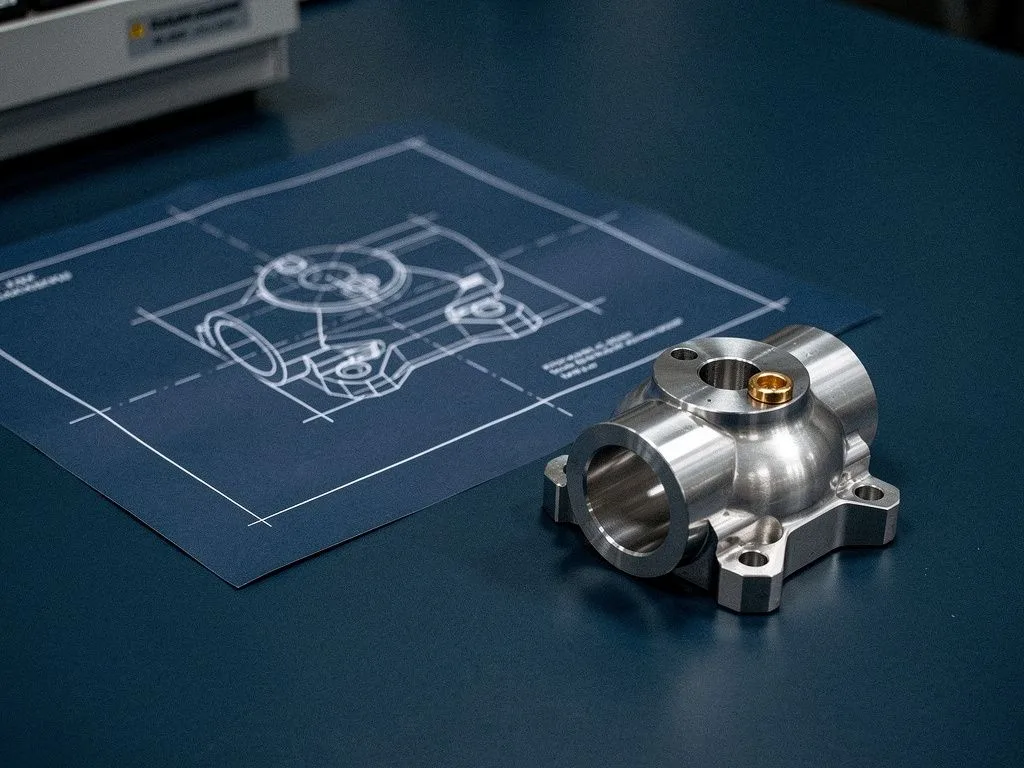
ysl-cnc surface-finishing-5

How to Specify Surface Treatment on Drawings and Acceptance Criteria

Surface treatment must be specified on drawings and acceptance criteria; otherwise, the machining shop can only rely on experience and guesswork, which often leads to disputes during the acceptance stage. Before placing an order, buyers should clearly mark on the engineering drawing the coating type, thickness, surface roughness, salt spray hours, and measurement locations, and state the inspection basis and sampling ratio in the purchase order. As a CNC machining shop, Yuan Shun Li executes the surface treatment specifications designated by the customer and performs final inspection before shipment, but the more complete the drawing information, the more accurate the quotation and delivery time.
Key Takeaways

  • Drawings must specify five surface treatment fields

    Coating type, coating thickness, surface roughness, corrosion resistance test conditions, and measurement locations allow the machining shop to get it right the first time and avoid acceptance disputes.

  • Acceptance requires six inspection criteria

    Coating thickness measurement, salt spray hours, appearance color difference, roughness and adhesion, sampling ratio, and inspection reports are all indispensable to protect the buyer's interests.

  • CNC precision and coating transition are easily overlooked

    Surface roughness affecting coating adhesion, tolerance and coating thickness sequence, and insufficient coating thickness in deep holes are the three details buyers most often overlook.

  • Write purchase order clauses in three sections

    Three sections covering specification reference, inspection methods, and non-conformance handling clearly assign responsibility when disputes arise and protect the buyer's interests.

Why Surface Treatment Specifications Must Be Written on the Drawing, Not Just in Emails or Verbal Instructions

If surface treatment specifications are only communicated via email or verbally, the machining shop often cannot implement them consistently during scheduling and material preparation. If it is only discovered before shipment that the coating type or thickness differs from expectations, rework or rejection becomes necessary. The drawing is the only document that is simultaneously reviewed by the CNC process, quality control, and shipping departments. Writing surface treatment specifications on the drawing ensures that after turning, milling, and five-axis machining, the coating and substrate combination matches the design when parts move to the next process. For buyers, the completeness of drawing annotations directly determines whether acceptance can pass in one go, and also determines whether the supplier bears responsibility in case of delivery delays. It is recommended that buyers clearly list the coating type code and corresponding international or industry standards, such as JIS, ASTM, or ISO numbers, in the technical requirements field in the lower right corner of the drawing, avoiding vague descriptions like "refer to attachment."

surface finishing scene 1

Which Surface Treatment Fields Should Be Marked on the Drawing So the Machining Shop Gets It Right the First Time

The surface treatment fields that should be marked on the drawing include at least five items: coating type name, coating thickness, surface roughness, corrosion resistance test conditions, and measurement locations. For the coating type name, it is recommended to use common codes, for example, "Type II or Type III" for anodizing aluminum alloys, "Type III hard" for hard anodizing, "Zn" for zinc plating, and "Ni" for nickel plating, avoiding in-house custom codes. The unit for coating thickness should be consistent, commonly μm or mil, and buyers should specify whether it is "minimum thickness" or "typical thickness," because the acceptance criteria for the two are completely different. The surface roughness Ra value should be written to one decimal place, for example, Ra 0.8 µm or Ra 0.4 µm, which is particularly critical when connecting the surface treatment layer to the CNC-machined surface roughness of Ra 0.3 µm. For corrosion resistance test conditions, the salt spray test hours and acceptance criteria should be clearly stated, for example, "neutral salt spray 96 hours, no red rust," which is the field most likely to cause disputes in the automotive and electronics industries. Measurement locations should be indicated on the drawing with arrows or dimension lines to prevent the machining shop from choosing measurement points on its own, which could lead to data deviations.
Six Inspection Criteria Buyers Should Prepare for the Acceptance Stage

  • Coating Thickness Measurement Basis

    Specify the coating thickness gauge brand and measurement point locations, and state whether it is "minimum" or "average," to prevent the machining shop from passing acceptance based on average values.

  • Salt Spray Test Hours and Judgment

    Write down the hours for neutral salt spray per ASTM B117 or JIS Z2371, and the judgment method such as "no red rust" or "white rust area less than X%."

  • Appearance and Color Difference Standards

    The color difference ΔE tolerance after anodizing should be written on the drawing; otherwise, color variations between batches will be rejected as defects.

  • Roughness and Coating Adhesion

    The Ra value after CNC machining and the coating adhesion test method (such as tape test or cross-cut test) should be specified together.

  • Sampling Ratio and Acceptance Quality Level

    State the AQL value and sampling quantity in the purchase order, for example, MIL-STD-105E Level II AQL 1.0, to avoid last-minute changes to acceptance criteria.

  • Inspection Reports and Shipping Documents

    Require the machining shop to include coating thickness reports, salt spray reports, and final inspection reports with the shipment; the electronics and automotive industries typically require one PDF and one paper copy.

Three details buyers most often overlook when connecting CNC machining accuracy with surface finishing

The connection between CNC machining accuracy and surface finishing is where buyers most often overlook details. The first detail is that post-machining surface roughness affects coating adhesion. For example, if the Ra value of aluminum alloy exceeds 0.8 µm before anodizing, coating uniformity will decrease. Therefore, if the drawing specifies Ra 0.4 µm, the machining shop must achieve this during CNC milling or turning, rather than leaving it for the surface finisher to correct. The second detail is the sequence of tolerances and coating thickness. If the critical dimension tolerance of a part is ±0.01 mm, a coating thickness exceeding 0.02 mm will push the part out of the tolerance band. In this case, the drawing must note "post-coating machining" or "pre-coating allowance." The third detail is internal and deep holes after multi-process machining. In these areas, chemical exchange is difficult during anodizing or electroplating, so coating thickness can easily be insufficient. Buyers should specify a minimum coating thickness inside deep holes on the drawing, or require the machining shop to perform sampling inspection with 3D CMM before shipment. Yuan Shun Li can achieve a precision tolerance of 0.007 mm in CNC turning, milling, five-axis, and multi-process machining, but the final dimensions after surface finishing must still be confirmed against the drawing specifications and the surface finisher's process capability.

Surface Treatment Quotation and Acceptance Process

  1. 1

    Specify surface treatment requirements on the drawing

    In the technical requirements field at the lower right of the drawing, specify coating type designation, thickness, roughness, salt spray hours, and measurement locations, and state the corresponding international or industry standards.

  2. 2

    Provide five items of quotation information

    The buyer provides five items: drawing, material, surface treatment specifications, batch quantity, and delivery schedule, so the machining shop can provide an accurate quotation and lead time.

  3. 3

    Write three-section clauses on the purchase order

    Write specification reference, inspection methods, and non-conformance handling as three sections, pre-agreeing on responsibility and handling procedures.

  4. 4

    Processing and final inspection before shipment

    The machining shop performs processing according to the customer-specified surface treatment specifications and conducts final inspections of coating thickness, salt spray, appearance, and other criteria before shipment.

  5. 5

    Attach inspection reports with shipment

    Require the machining shop to attach coating thickness reports, salt spray reports, and shipping inspection reports with the goods. The electronics and automotive industries typically require both PDF and paper copies.

surface finishing scene 2

How surface finishing clauses should be written on purchase orders to protect the buyer in disputes

Surface finishing clauses on purchase orders should be split into three sections—"specification reference," "inspection method," and "non-conformance handling"—to protect the buyer's rights in the event of a dispute. The specification reference section should state the drawing number, the version of the surface finishing standard, and the coating type code, for example, "Per drawing ABC-001 Rev. C, anodizing Type II, coating thickness 10–15 μm." The inspection method section should specify whether inspection is performed by the machining shop, a third party, or the buyer's resident inspector, and state the format and submission timing of the inspection report. The non-conformance handling section should pre-agree on the process and cost allocation for returns, rework, allowances, or scrapping, to avoid time-consuming negotiations afterward. For OEM and Tier-1 buyers, these three clauses are indispensable, because surface finishing defects are often only discovered after final product assembly. If the purchase order does not specify the handling method, the machining shop may claim that it has passed incoming inspection and in-process checks and refuse responsibility. Yuan Shun Li performs final inspection before shipment according to the inspection criteria specified by the customer, but the contractual allocation of responsibility must still be clearly defined by the buyer in the purchase order.

What information buyers should provide during the RFQ stage to get accurate surface finishing quotes from machining shops

During the RFQ stage, buyers should provide five items of information—drawings, material, surface finishing specification, order quantity, and lead time—so that the machining shop can give an accurate surface finishing quote. The drawings should include PDF and STEP or IGES files, allowing the machining shop to evaluate the CNC tool paths and the coating uniformity of the surface finish. The material should be specified as aluminum alloy 6061, 7075, or carbon steel S45C, because different materials require different chemical formulations for anodizing or electroplating, and the price difference can be as much as 30%. The surface finishing specification should include the coating type, thickness, salt spray hours, and color difference requirements. If the buyer only has functional requirements without specifying a coating type, the machining shop can only make recommendations based on experience, but the final choice remains with the buyer. Order quantity affects the surface finisher's minimum order quantity and unit price. For example, the minimum order quantity for anodizing is usually 100 pieces or more before the unit price enters a reasonable range. Lead time should be divided into the CNC machining cycle and the surface finishing cycle, as these are usually calculated separately. If the buyer only gives a total lead time, the machining shop may base the quote on the longer process. Yuan Shun Li accepts CNC machining orders from prototyping to mass production. Providing the above five items during the RFQ stage can speed up the quoting and sampling process.

Frequently Asked Questions

Why can't surface treatment specifications be communicated only by email or verbally?

Because email or verbal communication cannot be implemented consistently during scheduling and material preparation stages. If coating type or thickness is found to be non-conforming only before shipment, rework or rejection becomes necessary. The drawing is the document seen simultaneously by CNC processing, quality control, and shipping departments. Writing specifications into the drawing ensures the coating and substrate combination meets the design and passes acceptance on the first try.

Which surface treatment fields should be specified on the drawing?

At minimum, include five fields: coating type, coating thickness, surface roughness, corrosion resistance test conditions, and measurement locations. Use common designations for coating types such as Type II, Type III, Zn, Ni; unify thickness units as μm or mil; write Ra values to one decimal place; specify salt spray hours and acceptance criteria; and indicate measurement locations with arrows.

What inspection criteria should buyers prepare for acceptance?

Six criteria: coating thickness measurement basis, salt spray test hours and evaluation, appearance and color difference standards, roughness and coating adhesion, sampling ratio and acceptance quality level, and inspection reports and shipping documents. Each item must specify concrete values or standards, such as ASTM B117 or JIS Z2371, to avoid last-minute changes to acceptance standards.

What should be noted in the interface between CNC machining precision and surface treatment?

Three details: post-machining surface roughness affects coating adhesion, and coating uniformity decreases when Ra exceeds 0.8 µm; tolerance and coating thickness sequence, where coating thickness exceeding 0.02 mm may cause parts with ±0.01 mm tolerance to go out of tolerance; and deep holes and internal bores have poor chemical exchange, making coating thickness easily insufficient, so a minimum coating thickness or 3D CMM sampling inspection should be specified.

How should surface treatment clauses be written on purchase orders?

Split them into three sections: specification reference, inspection methods, and non-conformance handling. The specification reference section states the drawing number, standard version, and coating type designation; the inspection methods section notes whether inspection is in-house, by a third party, or resident at the factory; the non-conformance handling section pre-agrees on return, rework, allowance, or scrapping procedures and cost sharing to avoid time-consuming negotiations afterward.

Specify surface finishing requirements in your drawings to save time starting from the RFQ stage

If you are preparing drawings and purchase orders for CNC parts, we recommend fully specifying the surface finishing requirements before sending them out for quotation. You can send the drawings and technical requirements directly to [email protected], or call +886-4-2534-5219 to contact the Yuan Shun Li sales team, so that the CNC machining and surface finishing teams can evaluate lead time and costs simultaneously.